• Measure what matters

    Making food quality, freshness and product safety measurable

Solutions for the food industry

You know Konica Minolta as a provider of printing and document solutions. But our expertise goes further: With technologies for objective measurement and imaging quality control, we support food and beverage manufacturers in reliably monitoring quality, freshness and product safety along the entire value chain and detecting quality deviations at an early stage.
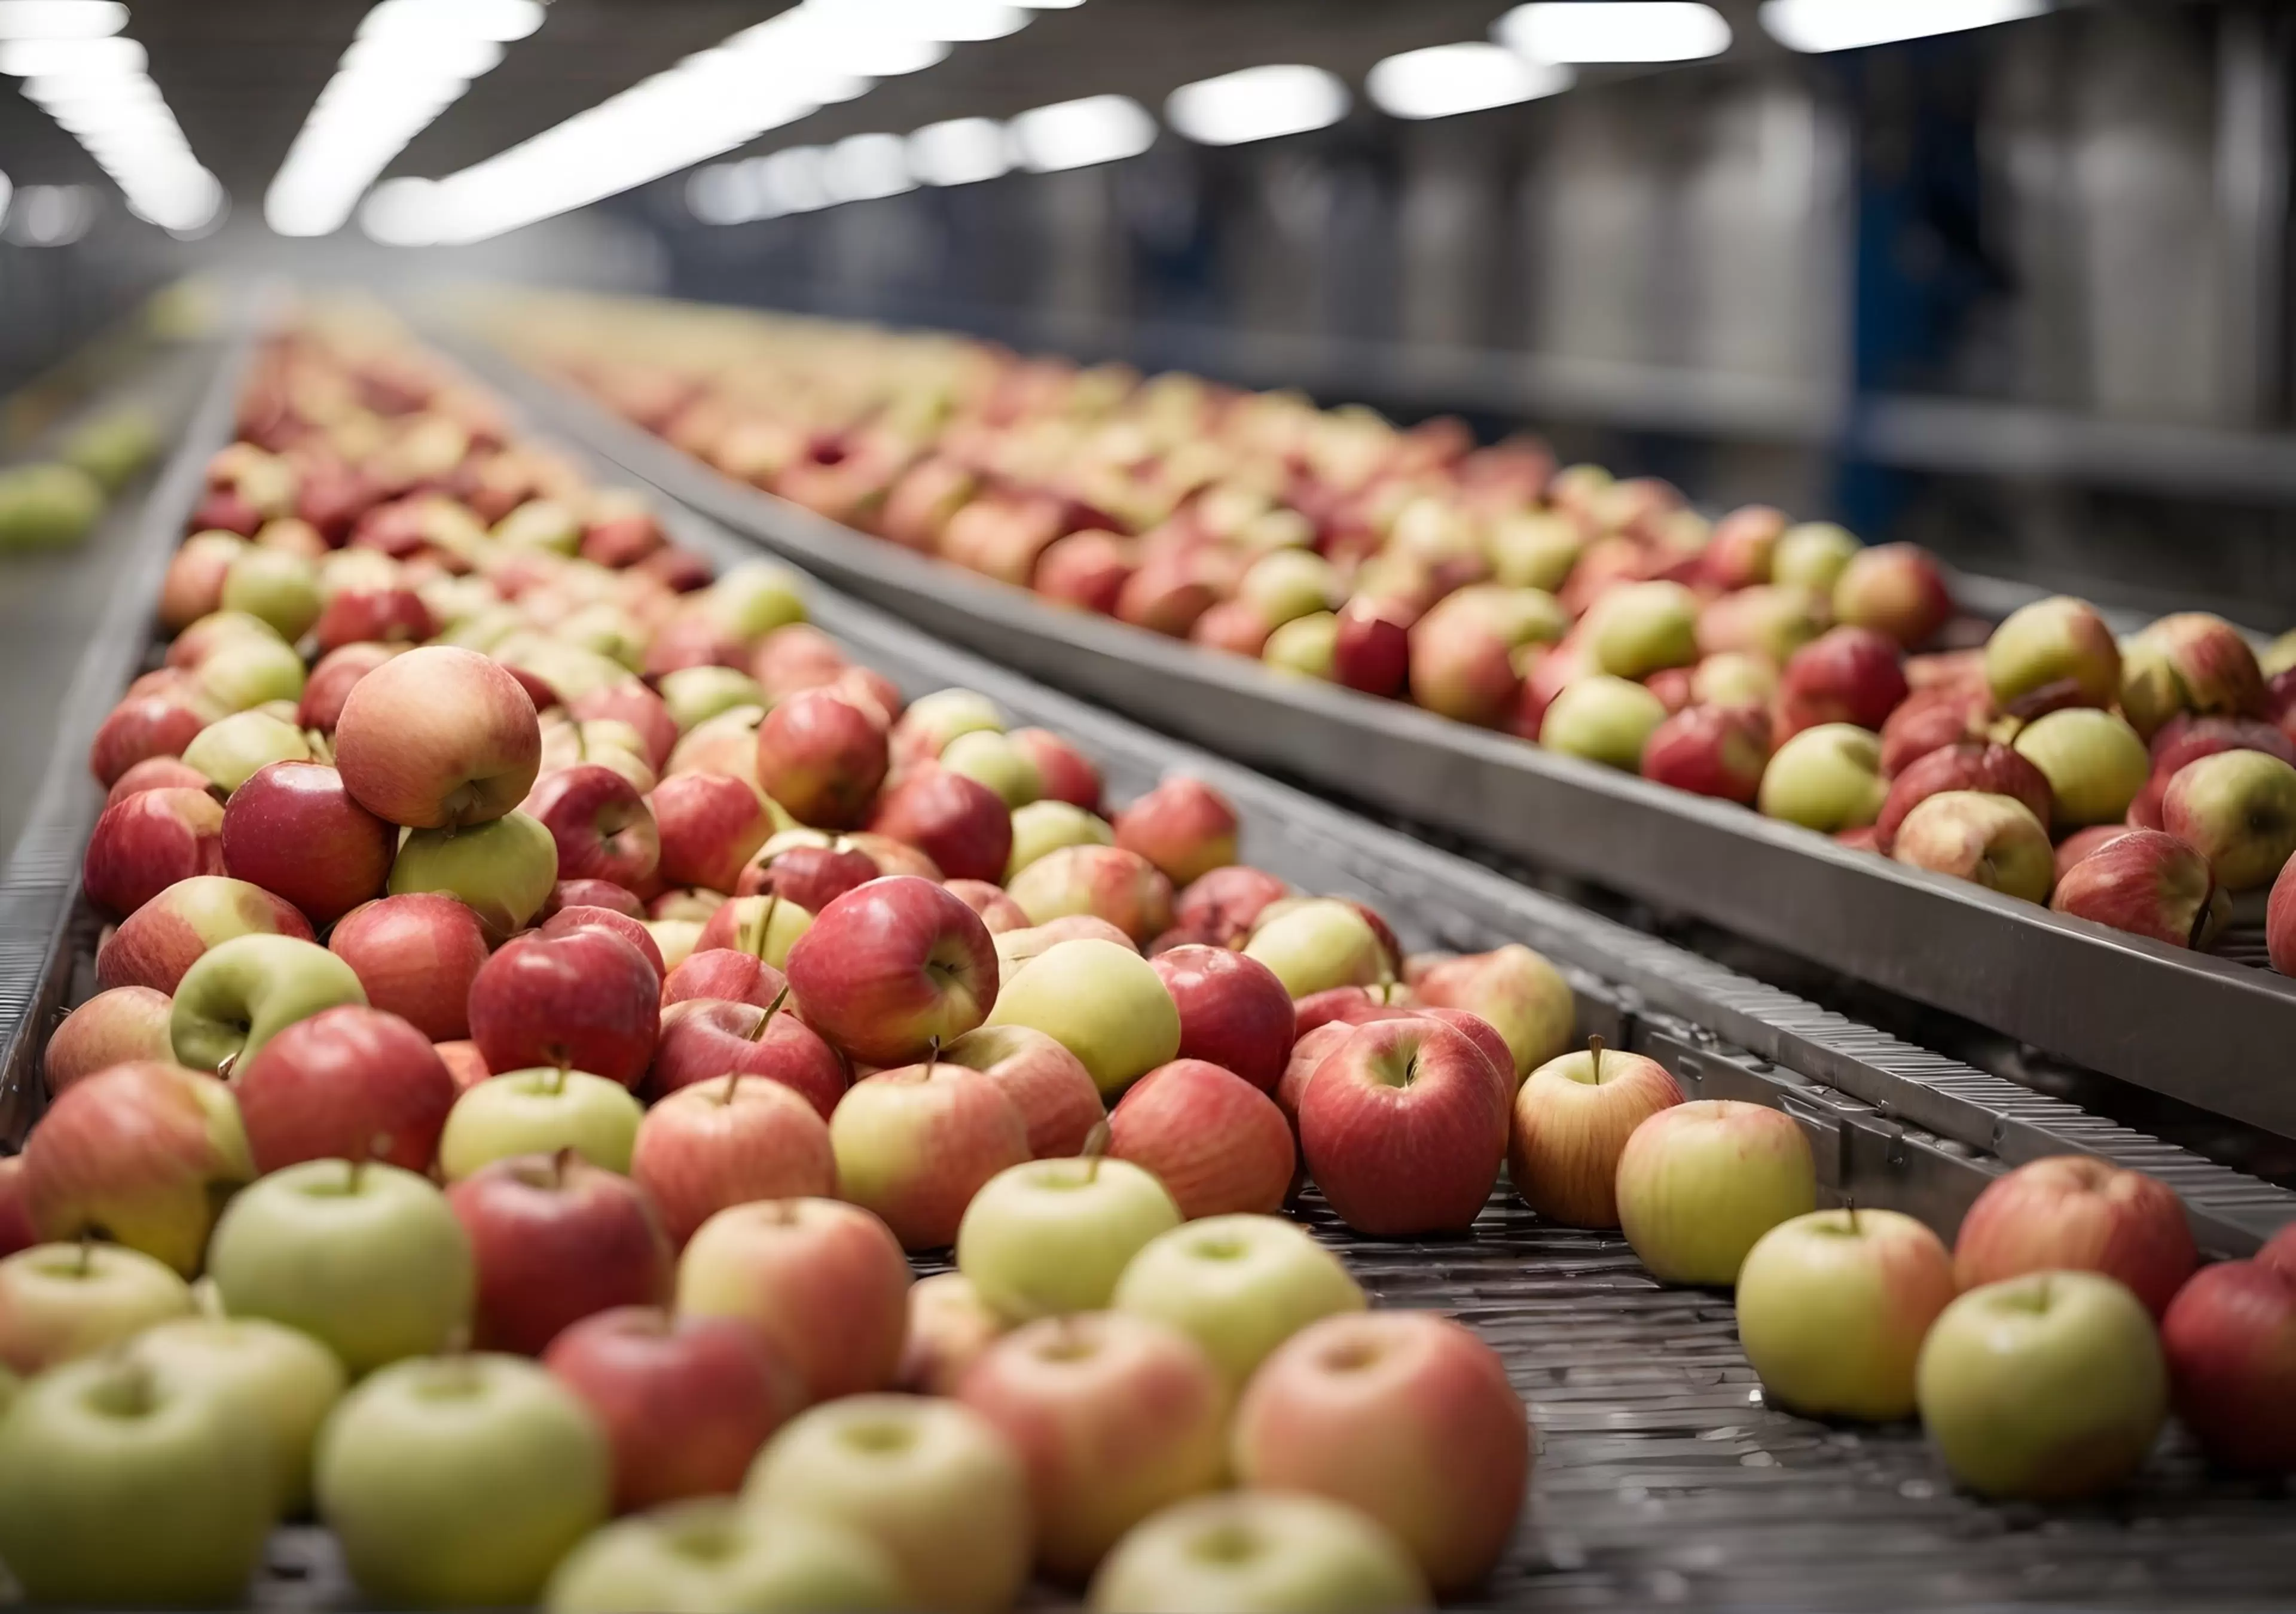
Clean and fresh gala apples on a conveyor belt in a fruit packaging warehouse for presize
food, manufacture, fruit, process, factory, agriculture, produce, conveyor, product, industry, safety, export, belt, sort, warehouse, line, technology, machine, equipment, plant, farm, fresh, machinery, goods, automatic, gala, modern, business, manual, packaging, logistics, harvest, crop, agricultural, manufacturing, domestic, apples, industrial, automated, robotic, production, processing, package, pack, facilities, grading, operating, rollers, sorting, washed

Fruits, Berries & Vegetables 

For fruits, berries and vegetables, measurement and imaging technologies help manufacturers to objectively evaluate colour, freshness, ripeness, even moisture and sugar content. Hyperspectral technology can be used to automate sorting, foreign body detection and optimise shelf life without slowing lines down. 
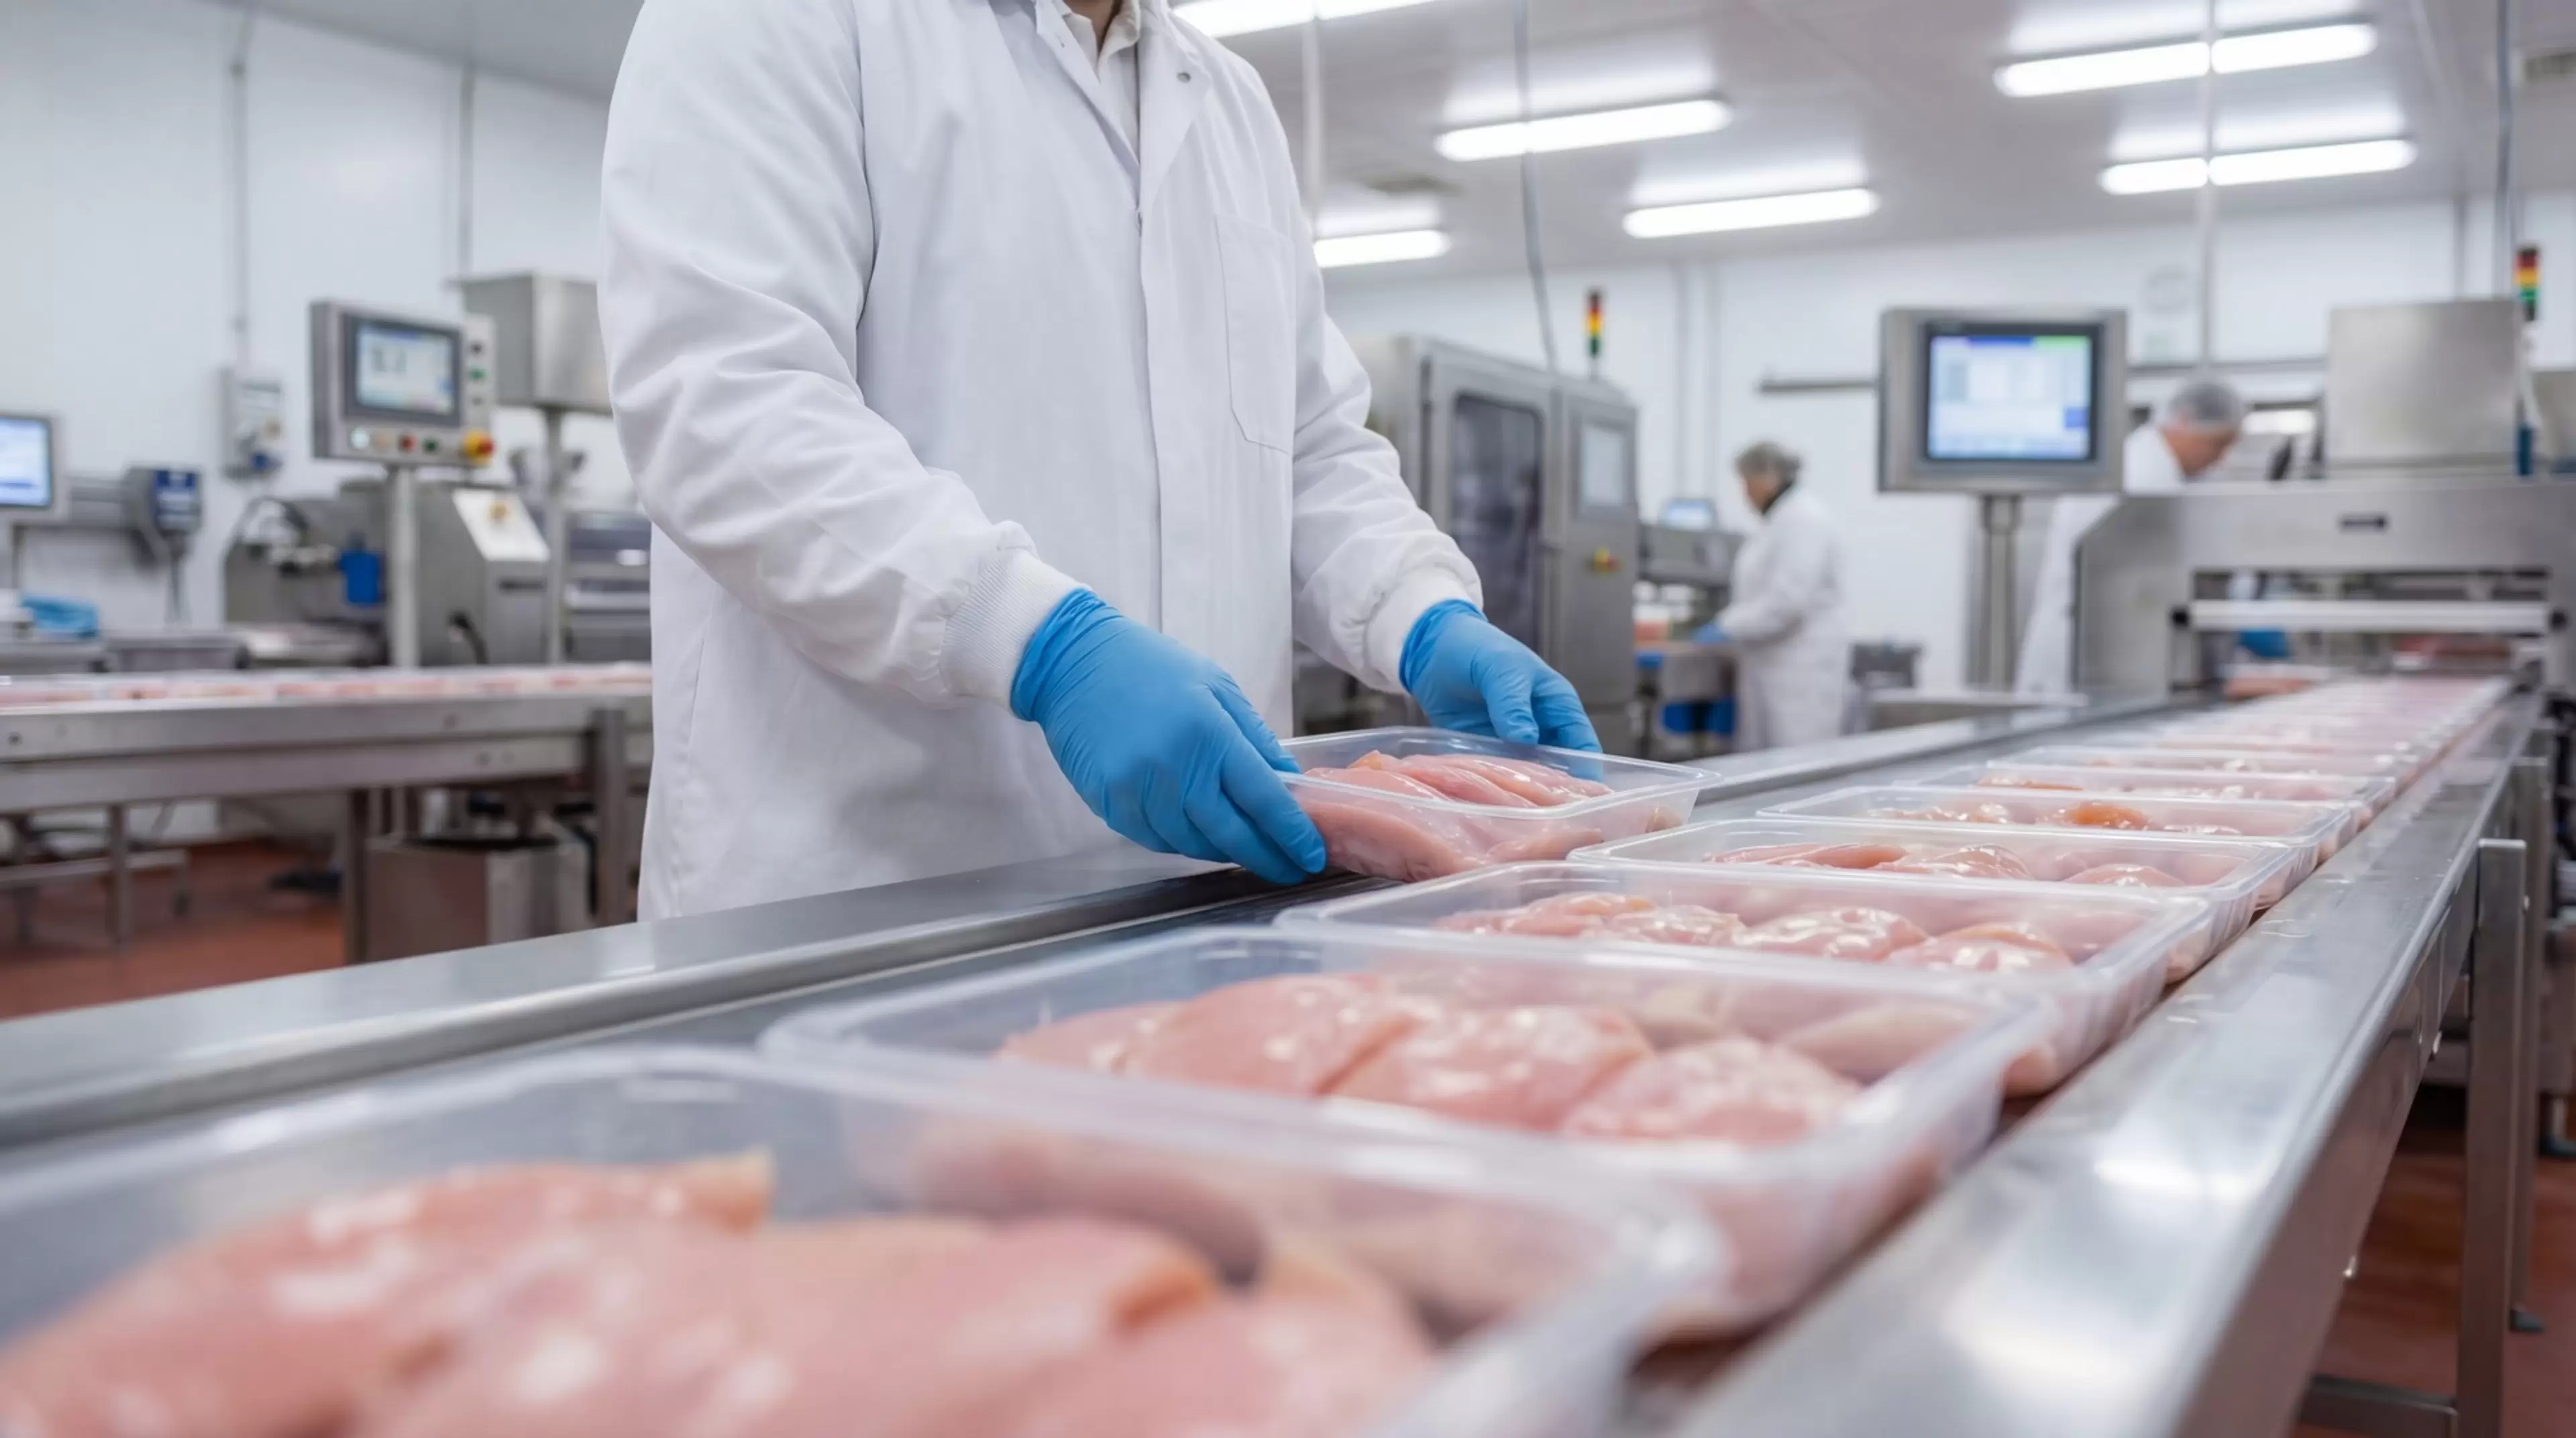
Worker inspecting packaged raw chicken breast fillets on industrial food processing and packaging line in modern poultry factory.
chicken, poultry, meat, raw, fillet, breast, packaging, processing, factory, production, line, manufacturing, conveyor, worker, employee, industry, food, plant, hygiene, sanitary, gloves, uniform, laboratory, quality, control, inspection, preparation, butcher, fresh, tray, plastic, packing, sorting, distribution, refrigerated, automation, machinery, industrial, facility, commerce

Meat, Fish & Poultry 

From detecting contaminants to evaluating freshness, moisture content, and fat percentage, hyperspectral imaging helps manufacturers detect quality deviations early, increase product safety, and ensure consistency in meat, fish, and poultry products.  
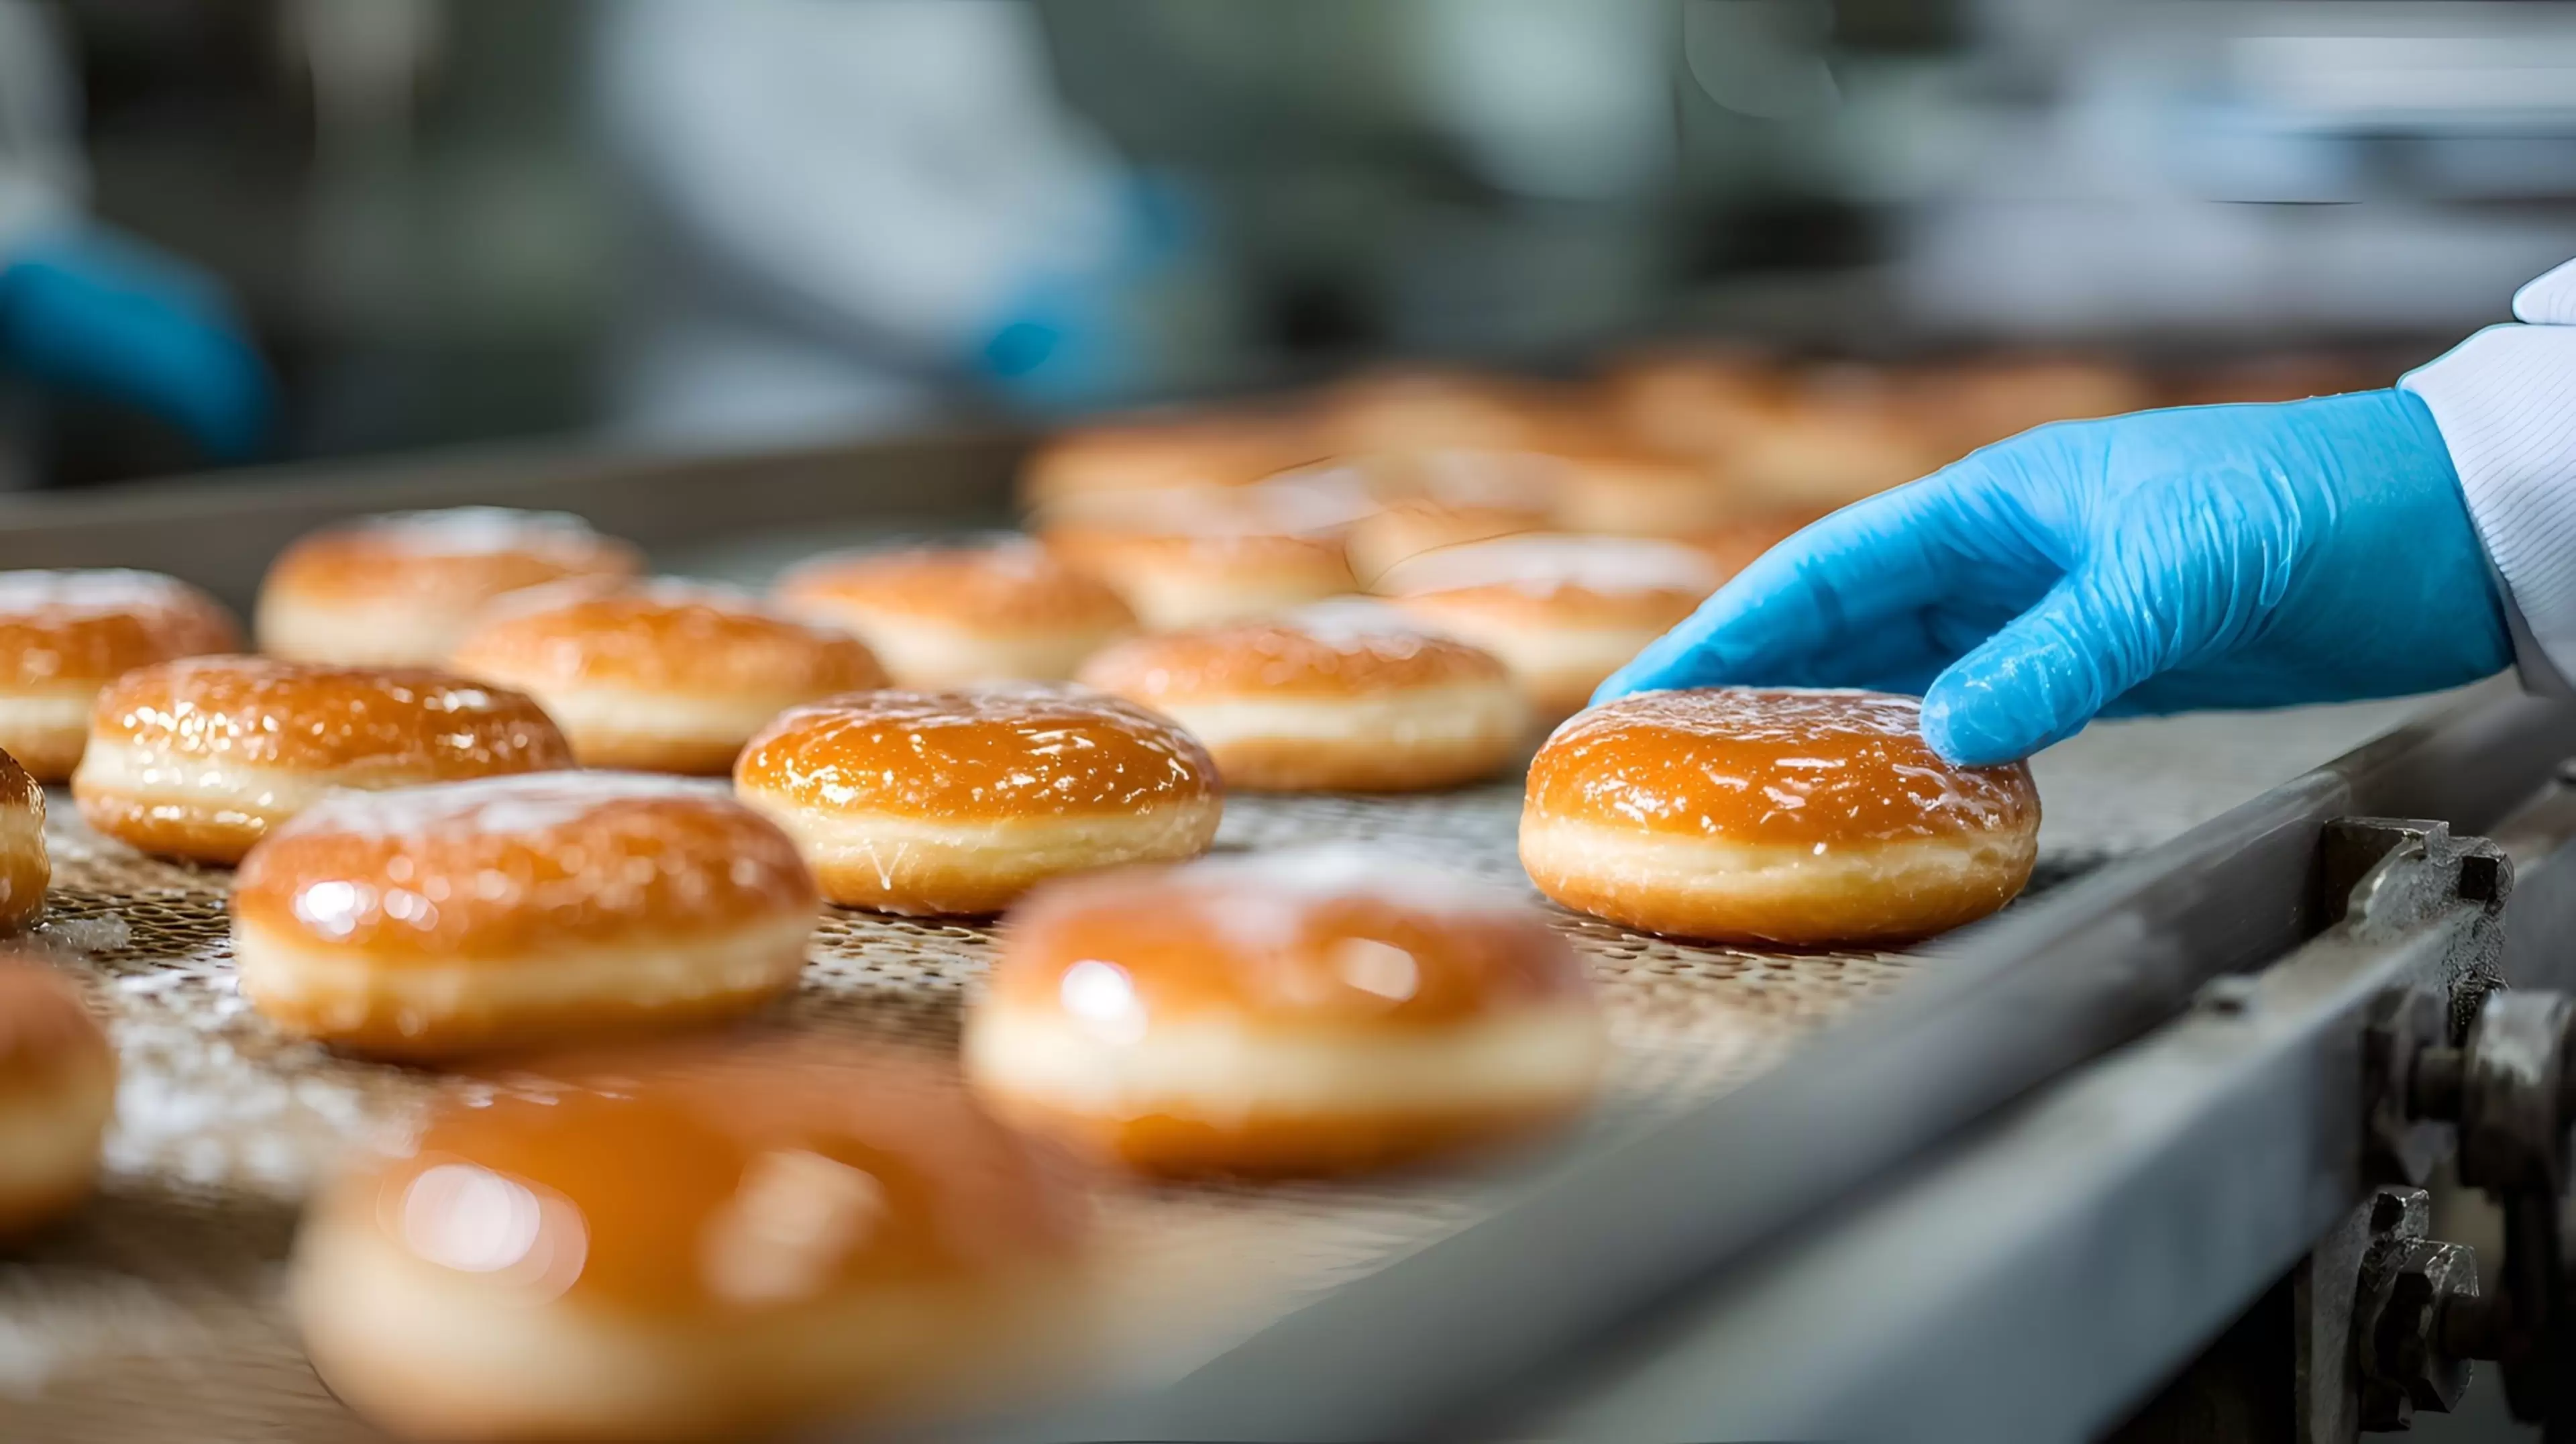
A factory worker in blue gloves inspects glazed donuts moving on a conveyor belt in a commercial food production facility environment..
A factory worker in blue gloves inspects glazed donuts moving on a conveyor belt in a commercial food production facility environment.

Bakery Products

From evaluating baking color and browning in bread and baked goods to analyzing product consistency and process changes. Objective measurement solutions help manufacturers meet quality standards, optimize production processes, and ensure consistently high product quality.
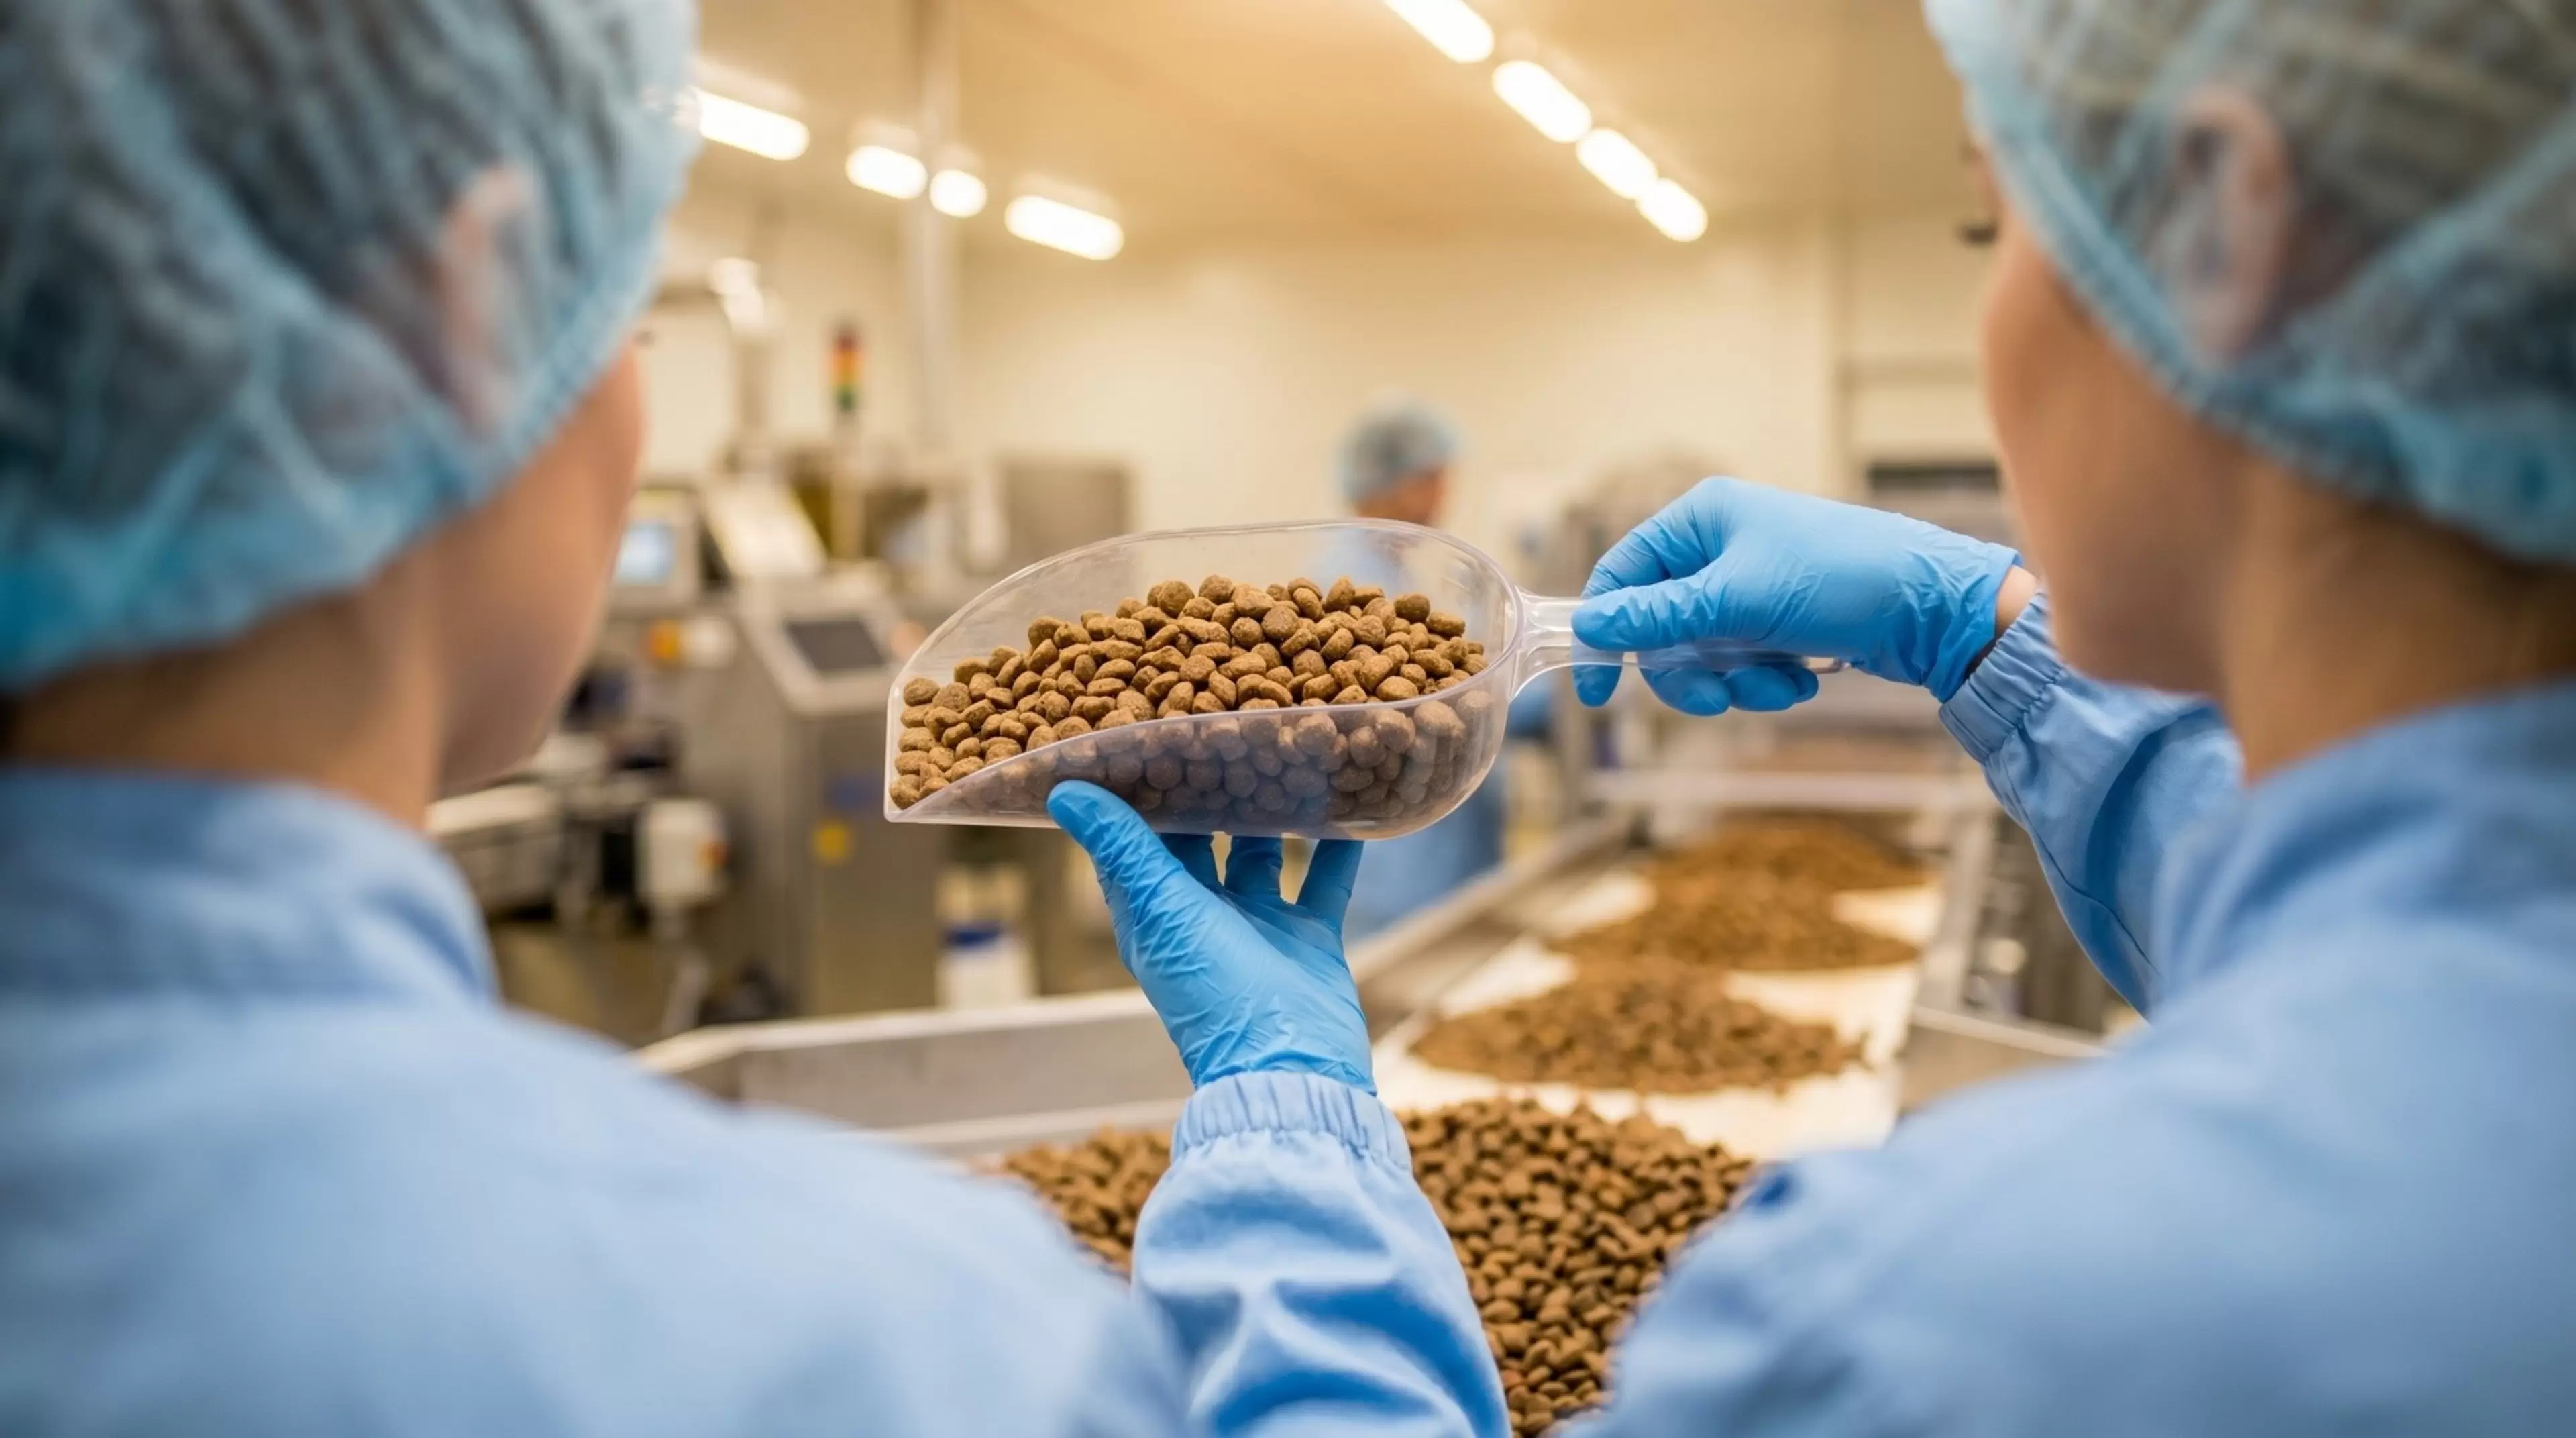
Opened ingredient

Powders, Grains, Nuts & Raw Materials 

From flour, milk powder, coffee and spice powders to grains, beans, legumes, nuts and granules: color measurement and hyperspectral imaging supports manufacturers in objectively evaluating quality characteristics and early detection of discoloration, mold or foreign bodies at. 
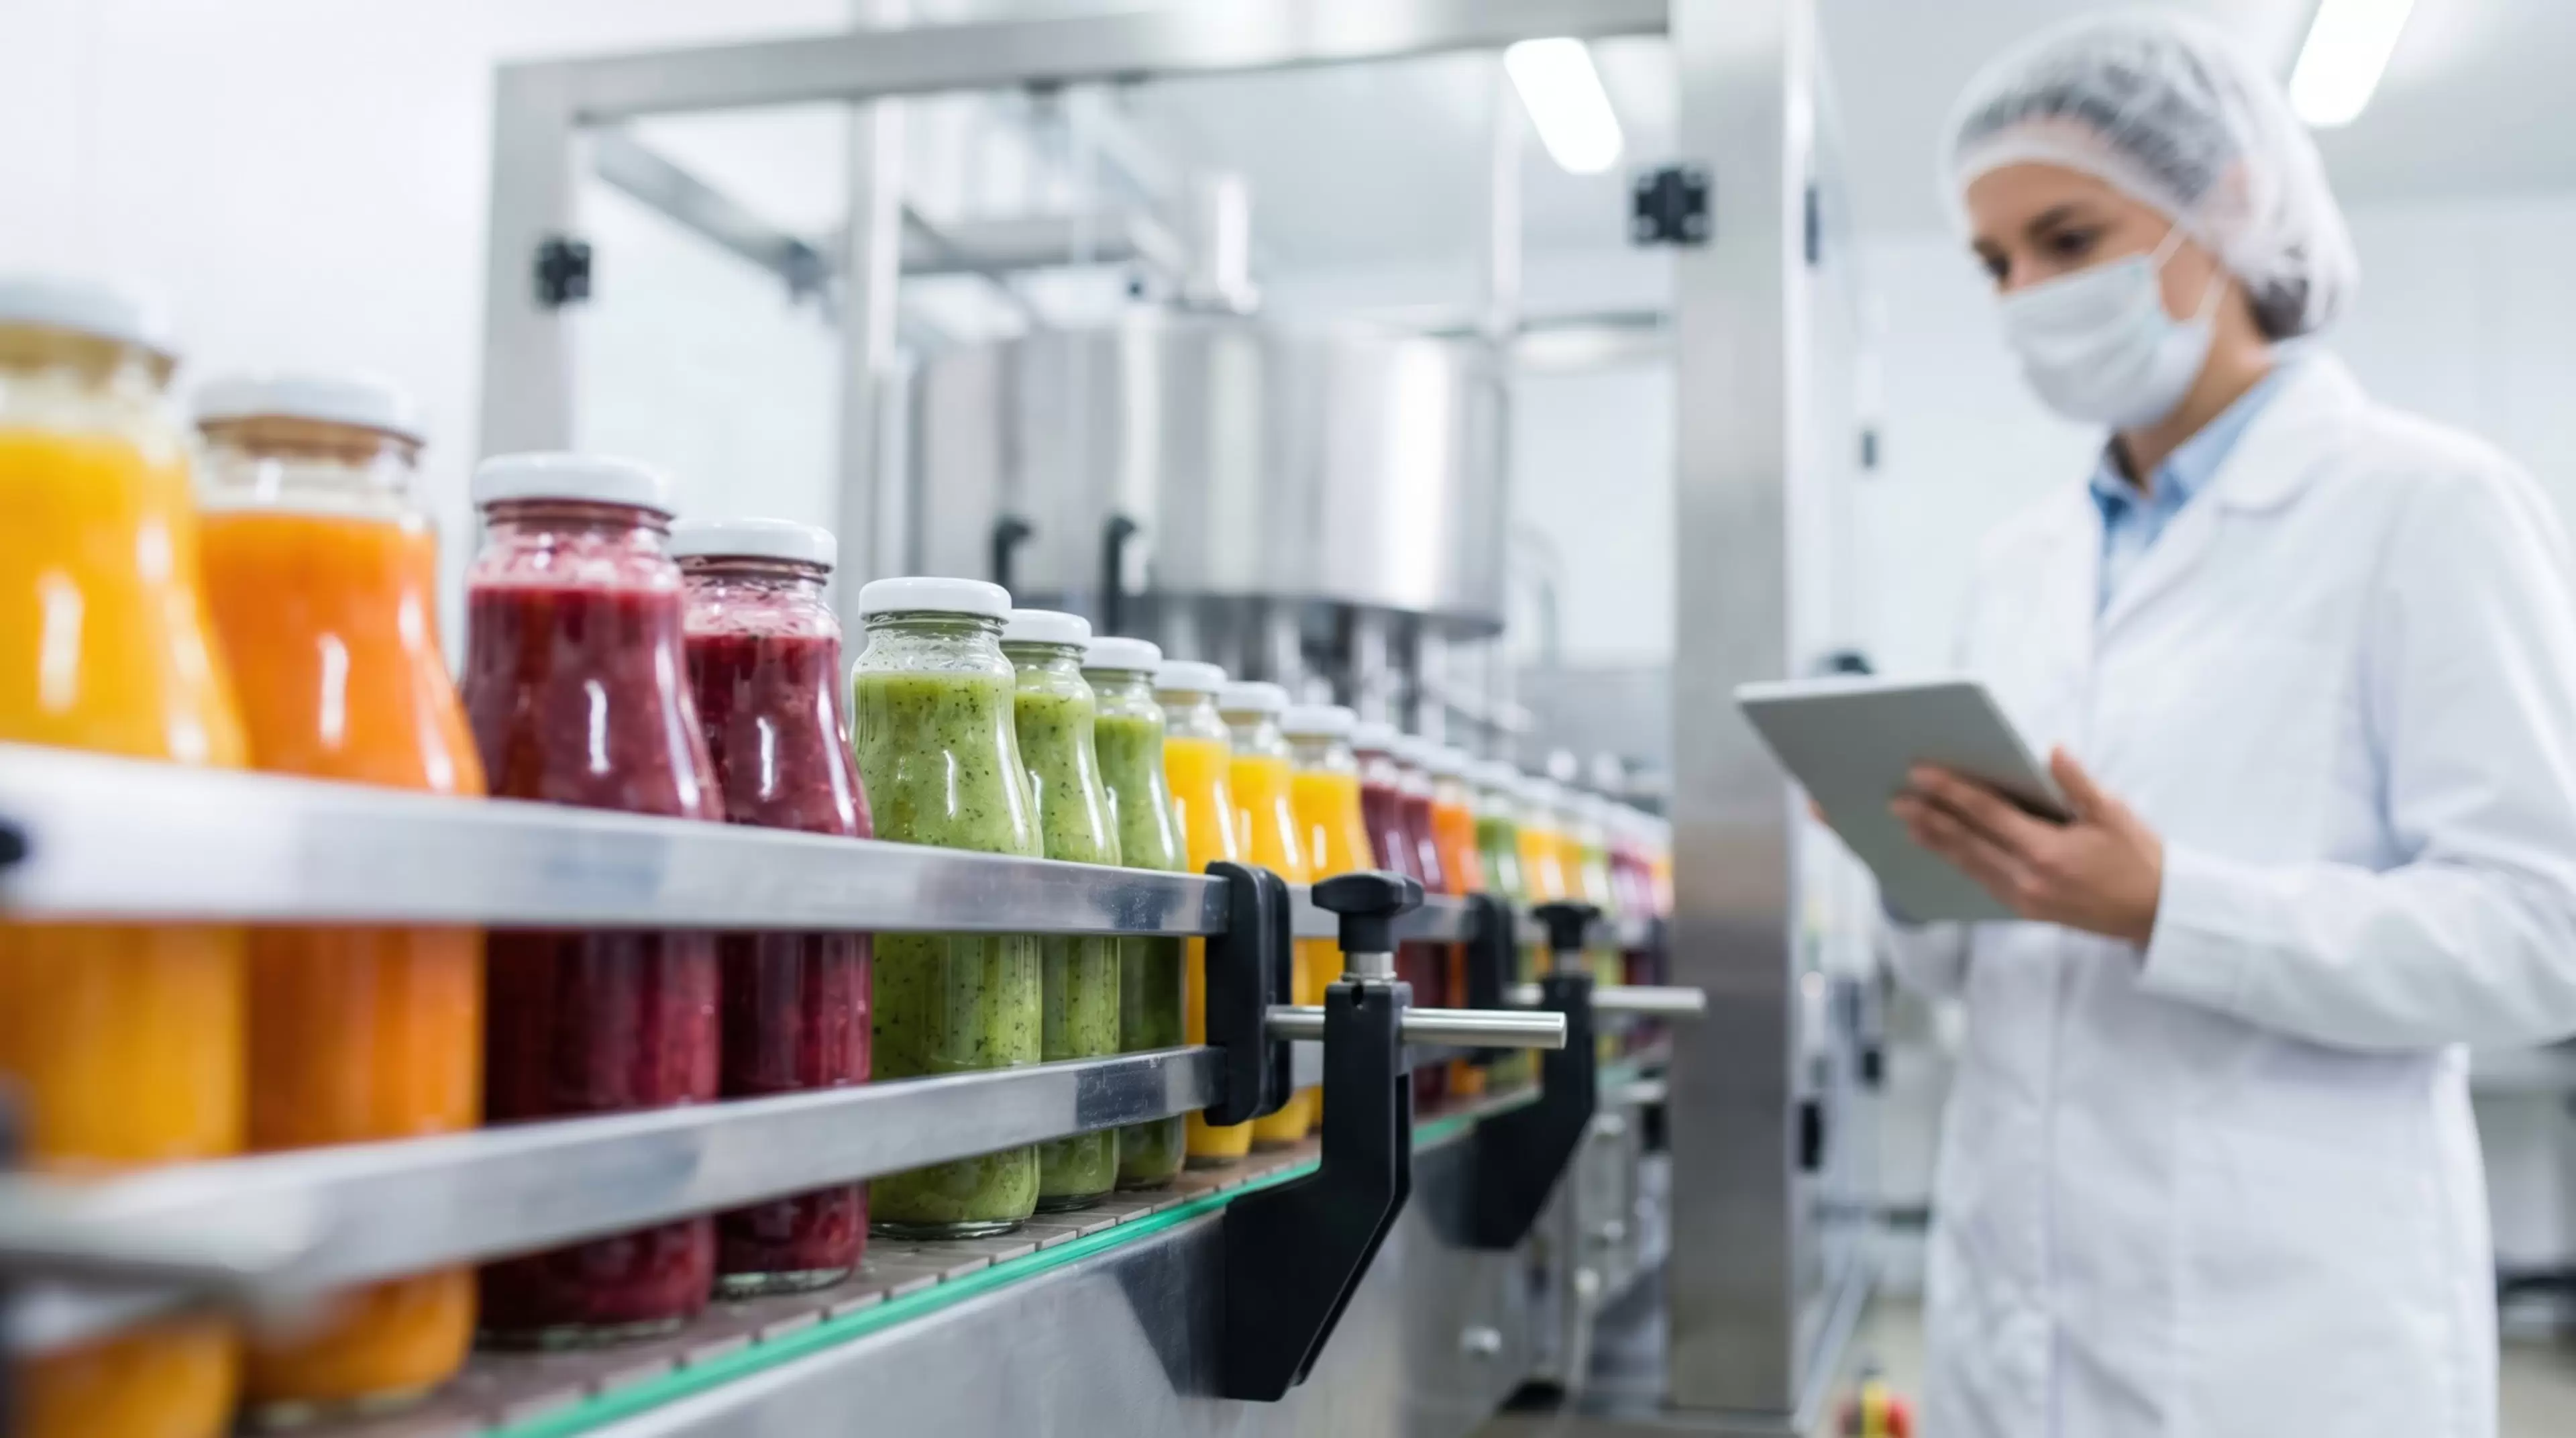
In a juice factory, a worker inspects bottles of various juices on a production line. The worker wears a lab coat, mask, and hairnet while using a tablet to monitor the process.
In a juice factory, a worker inspects bottles of various juices on a production line. The worker wears a lab coat, mask, and hairnet while using a tablet to monitor the process
food, production, industry, juice, factory, worker, bottles, quality, check, lab, coat, tablet, types, manufacturing, mask, hairnet, equipment, assembly, line, daytime, inspection, beverages, fruits, processing, technology, hygiene, workstation, floor, fresh, sweet, fruity, colorful, liquids, machines, bottling, standards, control, efficiency, labor, tasks, supply, chain, monitoring, operations, workflow, staff, process, supplies, inventory, readiness, services, task, management, tool, professional

Beverages & Liquid Food Products 

From juices, beer, and wine to dairy, syrups, and condiments, objective colour and quality measurements help manufacturers consistently evaluate color and haze, monitor production processes, and detect color variations early.

What quality features are crucial for your production?

Our experts will be happy to show you which solutions are suitable for your applications and processes.